Ricon Tools Ricon Tools

What Is the Maintenance for Quick Change Tool Holders?

Time:2026-09-28 Author:Sophia
0%

Quick-change tool holders keep turning operations moving by reducing setup time and helping operators repeat tool positions. Yet speed depends on more than the holder’s design. Chips, dried coolant, and a nicked locating surface can quietly affect seating and repeatability. A small problem. It can become a visible offset, extra scrap, or a tool that feels harder to lock. So, what maintenance do quick change tool holders need? The answer is practical: clean contact surfaces, inspect locking parts, lubricate only where specified, and verify fit regularly. Exact steps vary by holder type, machine, coolant, and duty cycle. The manufacturer’s instructions should guide maintenance intervals; a busy shop may need checks more often than a light-use cell. No single schedule fits every setup.

This guide explains routine care in clear shop-floor terms. It covers cleaning the holder and receiver, checking screws, pins, bushings, and clamping action, and spotting wear early. For example, a lint-free wipe can reveal a burr hidden under packed chips. A careful check. It also explains what to avoid: abrasive polishing, excess grease, or forcing a holder that does not seat smoothly may create new problems. These cautions matter because a holder can look clean while still failing to locate consistently. Maintenance records help connect symptoms with tool changes, but they are not magic. Operators should stop and consult the manufacturer when cracks, looseness, or unexplained runout appear. Some wear is subtle. The goal is reliable positioning and longer service life, not maintenance for its own sake.

What Is the Maintenance for Quick Change Tool Holders?

Identify the Components and Common Wear Points of Quick Change Tool Holders

What Is the Maintenance for Quick Change Tool Holders?

Identify the Components and Common Wear Points of Quick Change Tool Holders

A quick-change assembly typically includes a spindle-side holder, an adapter, a locking mechanism, and the cutting-tool interface. Some systems also use locating pins or coolant passages. Know the parts before inspecting them. Chips trapped on a coupling face can prevent full seating and create runout. Check the taper, contact faces, locking segments, and adapter for fretting, dents, rust, or uneven polishing. These marks often reveal repeated misalignment or poor cleaning.

Clean mating surfaces with a lint-free cloth and approved, non-abrasive cleaner. Never stone a precision face without proper training; removing material can worsen accuracy. Measure runout with a dial indicator, and compare results with the machine and holder specifications. Look closely at locking parts for cracks, burrs, or sluggish movement. Replace damaged components, rather than compensating with extra clamping force.

The U.S. Department of Energy’s Operations & Maintenance Best Practices guide reports broad plant-level benchmarks: predictive maintenance may reduce downtime by 35–45% compared with reactive approaches. Those figures are not specific to tool holders, but they support routine, documented checks. Records matter. Note wear, cleaning dates, and runout readings; visual inspection alone can miss gradual loss of repeatability.

Set an Inspection Routine for Holders, Clamps, and Interfaces

Inspect quick change tool holders on a regular schedule, and whenever a tool change feels rough or inconsistent. Stop the machine and follow its isolation procedure before handling components. Wipe the holder taper and mating interface with a clean, lint-free cloth. Look for embedded chips, dried coolant, burrs, fretting marks, or unusual discoloration. Small marks matter. Do not polish away damage without checking the holder’s service guidance.

Check clamps and locking elements for cracks, uneven wear, corrosion, and free movement. Test the mechanism by hand only when it is safe to do so. A clamp that sticks or closes unevenly can affect repeatability. Keep a simple record of inspection dates, observed wear, and any parts replaced. Photos can help compare changes over time. They are not a substitute for measurement.

Set the inspection interval to match actual use, contamination, and change frequency. A holder used daily in a chip-heavy environment may need closer attention than one used occasionally. Measure critical interfaces with suitable, calibrated tools, and compare results with the manufacturer’s limits. If runout rises or the holder no longer seats consistently, remove it from service for assessment. Check the mating spindle interface too; a clean holder cannot correct a damaged seat. Routines can become rushed, so leave space for an honest note when an inspection was incomplete.

Quick-Change Tool Holder Maintenance: Suggested Inspection Routine

Suggested maximum intervals between checks, in operating hours.

Clean the holder and mating interface each shift. Inspect gripping surfaces and check seating, wear, and runout regularly; verify clamp force and service the mechanism at longer intervals. These are practical starting points, not universal limits—follow the holder manufacturer’s instructions and adjust for operating conditions.

Clean the Holder and Remove Chips, Coolant, and Residue

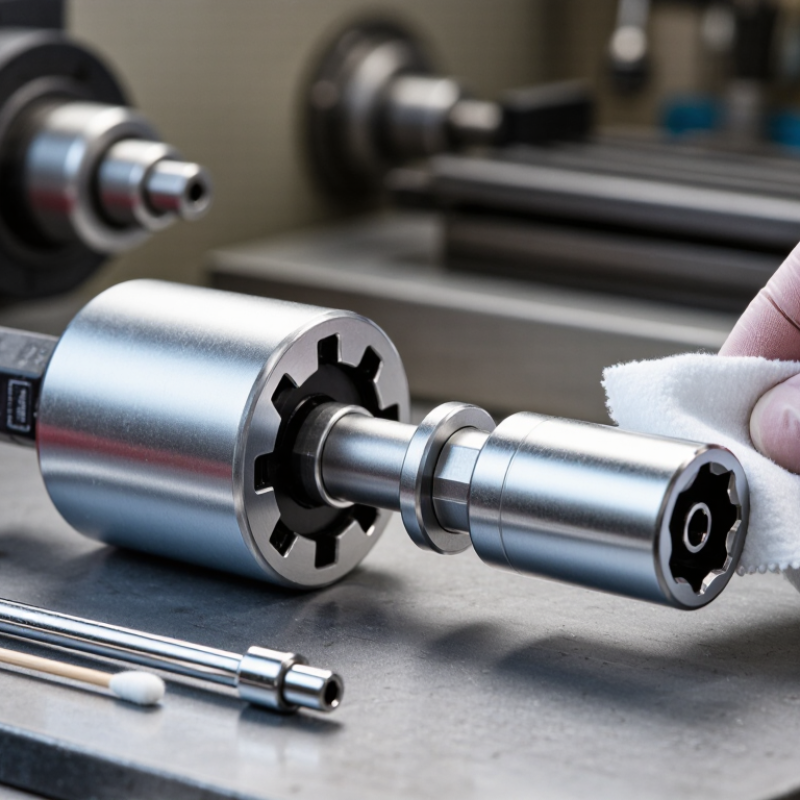
After safely stopping the machine, remove the tool and inspect the holder under good lighting. Wipe away loose chips with a clean, lint-free cloth. Small particles matter. A chip trapped near a locating surface can affect seating and contribute to runout. Use a soft nylon brush for debris in recesses, then check the holder’s taper, clamping area, and accessible grooves. Avoid knives, abrasive pads, or stiff wire brushes; they can scratch precision surfaces. Keep cleaning tools free of grit, too.

Coolant and oil can leave a thin film that attracts more chips. Apply a cleaner suitable for the holder material to a cloth, rather than flooding the assembly. Follow the equipment maker’s care instructions, and dry all surfaces completely before reinstalling the tool. Do not rush. A surface may look clean while residue remains near a shoulder or groove, so inspect it from more than one angle. If buildup will not lift with gentle cleaning, pause and check the service guidance instead of scraping harder. Regular cleaning after use, or whenever visible contamination appears, makes damage easier to spot.

Lubricate Moving Parts and Check Clamping Force

Quick-change tool holders work best when their moving parts stay clean and lightly lubricated. Before servicing, remove the holder from the machine and follow its maintenance instructions. Wipe exposed sliding surfaces with a lint-free cloth, then apply a small amount of the specified lubricant to the contact points. Too much grease attracts fine chips and dust. Keep lubricant off the taper and clamping surfaces unless instructions specifically allow it. Move the mechanism through its full travel several times, then wipe away excess. A sticky feel deserves attention; forcing the mechanism can hide wear. In a busy shop, routine cleaning is easy to skip, and that small delay can make later inspection harder.

Check clamping force at the interval recommended for the holder and spindle system. Use a suitable force gauge, and compare readings with the stated operating range. Record the result, date, and any unusual variation. A declining reading may point to worn components, contamination, or an adjustment issue, not simply a need for more lubricant. Never compensate by tightening beyond the specified limit. If force is inconsistent, or the holder slips during a controlled check, take it out of service for inspection. Check again after cleaning or component replacement.

Replace Worn Components and Verify Safe Tool Retention

Quick change tool holders need routine inspection, especially when tools are changed many times per shift. Isolate the machine before removing a holder, then wipe away chips and coolant with a clean, lint-free cloth. Check the taper, locating surfaces, locking segments, and retention balls for scoring, cracks, or uneven wear. A small burr can prevent full seating. Small signs matter.

Replace worn springs, locking parts, seals, or other serviceable components with parts specified for that holder. Do not mix components from different assemblies; slight differences can affect clamping force. Follow the service instructions for disassembly and reassembly, and keep parts clean as you work. Do not guess. If a component’s condition is unclear, compare it with the manufacturer’s wear limits or ask a qualified technician. A faint click can be misleading.

After maintenance, confirm that the holder moves freely and locks fully. Use the approved retention test or gauge for the holder and machine; a hand tug alone cannot prove secure clamping. Check that the tool seats squarely, with no visible gap or rocking. Run the machine only after the holder passes the prescribed checks, starting under controlled conditions. Record replaced parts and test results. It may feel tedious, but a quick note can reveal recurring wear before it becomes a safety problem.

What Is the Maintenance for Quick Change Tool Holders? — Replace Worn Components and Verify Safe Tool Retention
Maintenance Area Suggested Check Frequency What to Inspect Maintenance Action Safe Condition to Verify
Holder body and locating surfaces Before use; clean after machining or when contamination is visible Look for cracks, dents, corrosion, burrs, and embedded chips on the holder and its locating surfaces. Clean with a lint-free cloth and an approved cleaning method. Remove a damaged holder from service; do not grind or alter precision locating surfaces. Surfaces are clean and undamaged, and the holder seats correctly in its intended interface.
Quick-change locking mechanism Before use and during routine setup checks Check the release sleeve, latch, locking balls or other retention parts for smooth movement, damage, looseness, or contamination. Clean and lubricate only as directed by the holder or machine manufacturer. Replace worn or damaged retention components with compatible parts. The mechanism moves freely, locks fully, and does not release under the manufacturer’s specified retention test.
Tool shank and holder contact surfaces At every tool change Check the tool shank and mating surfaces for chips, oil buildup, scoring, wear, or damage that could prevent full seating. Clean both mating surfaces. Remove tools with damaged shanks from service; do not force a tool into a holder that does not seat properly. The tool is fully seated and the locking mechanism engages without unusual force.
Retention components and replaceable wear parts At scheduled maintenance intervals and whenever retention performance changes Inspect replaceable pins, balls, springs, collets, sleeves, or other model-specific parts for wear, deformation, or breakage. Replace parts that are worn, damaged, or outside the manufacturer’s service limits. Use the specified component type and assembly procedure. All components are correctly installed, and the holder retains the tool as specified by its manufacturer.
Coolant and chip passages After use in chip-producing or coolant-heavy operations; otherwise as needed Check passages and seals for blockage, leaks, damage, or accumulated chips and residue. Clear passages using an approved cleaning method. Replace damaged seals and avoid methods that could injure the operator or damage the holder. Passages are clear and any required coolant delivery is unobstructed and leak-free.
Tool-retention verification After assembly, component replacement, or any retention concern Confirm that the correct tool and holder are installed and that the locking feature has fully engaged. Perform the manufacturer’s specified retention or pull-out check when required. Keep hands clear of moving parts and follow machine lockout and guarding procedures. The tool remains securely retained during the prescribed check; do not run the machine if retention is uncertain.
Storage and handling After use and before storage Check that holders are protected from impact, moisture, chips, and contact with abrasive debris. Clean and dry holders, then store them in a suitable rack or case with precision surfaces protected. Holders are stored cleanly without risk of damage or contamination before the next use.

Note: Inspection intervals and acceptance limits depend on the holder design, application, and operating conditions. Follow the manufacturer’s instructions and applicable machine-safety procedures; remove any holder with uncertain tool retention from service.
FAQS

What parts should I inspect on a quick-change tool holder?

Check the spindle-side holder, adapter, locking mechanism, and cutting-tool interface. Some assemblies also have locating pins or coolant passages.

Which signs may indicate wear or poor alignment?

Look for fretting, dents, rust, uneven polishing, cracks, or burrs. These marks can point to misalignment, wear, or poor cleaning.

How should I clean the holder?

Stop the machine and remove the tool. Wipe surfaces with a lint-free cloth and use a soft nylon brush for recesses. Small chips matter.

Can I scrape or polish stubborn residue from a precision surface?

Avoid knives, abrasive pads, and unapproved polishing. If gentle cleaning fails, pause and check the service instructions. Scraping harder may cause damage.

How can I check runout?

Measure it with a dial indicator and compare the reading with machine and holder specifications. Record results to spot gradual changes.

Where should lubricant be applied?

Apply a small amount of specified lubricant to moving contact points. Keep it off tapers and clamping surfaces unless instructions allow it. Too much attracts chips.

How do I check clamping force?

Use a suitable force gauge at the recommended interval. Compare readings with the stated range, and record the date and result.

What should I do if clamping force is inconsistent?

Remove the holder from service and inspect it. Contamination or worn parts may be responsible. Do not exceed the specified tightening limit. A quick fix can mislead.

Conclusion

Quick change tool holders require regular maintenance to remain accurate, secure, and reliable. Begin by identifying the holder’s main components and likely wear points, including clamping elements, contact surfaces, and interfaces. Set a consistent inspection routine, checking for cracks, damage, looseness, corrosion, or unusual wear before use. Keeping a record of inspection results can help reveal changes over time and indicate when parts need attention.

To understand what maintenance do quick change tool holders need, keep the holder clean by removing chips, coolant, and residue from its surfaces and interfaces. Lubricate moving parts as recommended for the holder, and check that the clamping action and force are appropriate. Replace worn or damaged components promptly, then verify that the tool is retained securely before returning the holder to service.

Sophia

Sophia

Sophia is a dedicated marketing professional with an exceptional depth of knowledge about her company's products and services. With a keen understanding of market trends and customer needs, she crafts insightful blog posts that not only inform but also engage readers, enriching the company’s online......